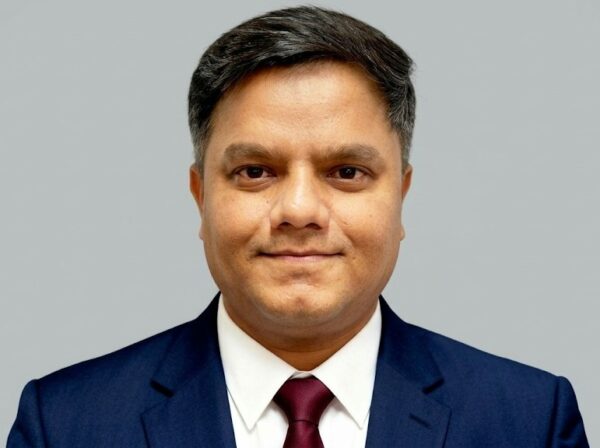
In pharmaceutical manufacturing, product quality depends not only on the ingredients used but also on the environment in which medicines are produced. While temperature control often receives considerable attention, humidity and moisture management are equally important for ensuring product stability, manufacturing consistency and operational efficiency. In this interview with Samuel Dike, Anup Sharma, regional head for West Africa at Bry-Air Nigeria Limited, discusses the importance of humidity control, the environmental challenges facing Nigerian pharmaceutical manufacturers, and how modern dehumidification and air-treatment technologies can improve product quality, energy efficiency and manufacturing performance. Excerpts.
Why is humidity as important as temperature in pharmaceutical manufacturing?
Temperature and humidity are equally important in maintaining a controlled pharmaceutical manufacturing environment. While temperature influences reaction rates, product stability and processing conditions, humidity directly affects the moisture content of raw materials, powders, granules, tablets and capsules. Many pharmaceutical ingredients absorb moisture from the surrounding air, potentially becoming sticky, forming lumps and affecting accurate dosing and tablet compression.
Conversely, excessively low humidity can generate static electricity, creating difficulties in powder handling and filling operations. Humidity control is therefore not merely an HVAC requirement; it is a critical process parameter that influences product quality, manufacturing consistency and operational efficiency.
What are the consequences of inadequate humidity control?
Poor moisture control can affect pharmaceutical production at every stage, from raw material storage to final packaging. Moisture-sensitive ingredients may deteriorate, while powders can form lumps, obstruct equipment and flow inconsistently. Variations in moisture content can also affect tablet compression, hardness, disintegration, coating uniformity and filling operations.
During storage and packaging, moisture absorption may compromise product stability and shelf life. These problems can lead to rejected batches, production downtime, rework and additional quality investigations. Manufacturers must therefore establish humidity requirements based on the specific product, manufacturing process and applicable Good Manufacturing Practice (GMP) requirements.
What are the limitations of conventional HVAC systems when precise humidity control is required?
Conventional heating, ventilation and air conditioning (HVAC) systems are designed primarily to regulate temperature, provide ventilation and maintain general indoor environmental conditions. Although they can control humidity within certain limits, maintaining very low and stable humidity levels can be challenging, particularly in tropical climates. Cooling-based dehumidification may require substantial cooling followed by reheating, thereby increasing energy consumption.
Desiccant dehumidification offers an alternative by removing water vapour through adsorption, making it suitable for applications requiring low dew points or precise humidity control. In many pharmaceutical facilities, integrating a properly designed desiccant system with existing HVAC infrastructure can provide a more effective solution than replacing the entire system.
How can modern dehumidification technologies improve energy efficiency?
Modern dehumidification systems can be integrated with cooling coils, heat recovery systems, variable-speed drives and intelligent controls. Depending on the application, these technologies can reduce unnecessary cooling and reheating, reuse suitable waste heat for desiccant regeneration, and improve the management of ventilation and moisture loads.
However, energy savings depend on factors such as climate, required humidity levels, process moisture loads, equipment selection and operating strategy. Manufacturers should assess the total energy consumption of a proposed system rather than focus solely on equipment power ratings. The objective is to maintain the environmental conditions required for product quality while achieving the lowest practical total energy consumption.
What industry challenges have driven Bry-Air and DRI to develop these technologies?
The growing need for precise process control, product protection, energy efficiency and reliable manufacturing has driven the development of advanced dehumidification and air-treatment technologies. Pharmaceutical manufacturers must protect moisture-sensitive ingredients and maintain consistent environmental conditions during powder processing, filling, coating and packaging. Other industries, including food, electronics, chemicals and lithium-ion battery manufacturing, also require specialised environmental conditions.
Bry-Air addresses these needs through technologies covering dehumidification, air purification, heat recovery, cooling and other environmental-control solutions. Since no single HVAC configuration can meet the requirements of every industry, each application demands a clear understanding of the product, manufacturing process, moisture load and required environmental conditions.
What specific problems are Bry-Air’s pharmaceutical solutions designed to address?
Bry-Air’s pharmaceutical solutions address moisture-related challenges across different stages of manufacturing, including cleanrooms, powder milling, tablet compression and coating, capsule production, dry injection and vial filling, as well as the storage of raw materials and finished products. Excess moisture can make powders difficult to handle, disrupt filling operations and affect the consistency of pharmaceutical products.
Humidity management is also important during packaging and storage, particularly for moisture-sensitive medicines and hygroscopic products. The objective is to maintain the environmental conditions required for each process while supporting product consistency and operational reliability. The appropriate solution depends on the specific requirements of the manufacturing application.
What are the major environmental-control challenges in Nigeria and other tropical markets?
One of the biggest challenges in Nigeria is the combination of high outdoor humidity, elevated temperatures and the substantial moisture introduced into manufacturing facilities through fresh air. A production room may reach its target temperature while its relative humidity remains above the required limit, particularly during humid weather.
Other challenges include poor insulation, air leakage, inadequately sealed rooms, insufficient preventive maintenance and HVAC systems that are not designed to meet specific production requirements. Manufacturers must consider the building structure, production process, airflow, filtration, equipment, controls and maintenance practices. Environmental control should be approached as an integrated engineering solution rather than simply an equipment purchase.
How can manufacturers balance sophisticated environmental control with energy and cost efficiency?
Manufacturers should design environmental-control systems around actual production requirements rather than over-engineer an entire facility. This begins with establishing the temperature and humidity limits required for each production area, calculating the moisture load and selecting suitable technology. Separate environmental-control zones, energy recovery, calibrated sensors and automated controls can also help improve efficiency.
It is equally important to consider the total cost of ownership, including electricity, maintenance, spare parts, production interruptions, product rejection and equipment lifespan. A higher initial investment may offer better long-term value if it improves reliability and reduces production losses. The best solution is one that consistently meets process requirements at the lowest reasonable life-cycle cost.
What is the future of humidity-control technology in pharmaceutical manufacturing?
The future of air-treatment technology lies in more intelligent, integrated and energy-efficient environmental-control systems. Sensors and data analytics can help manufacturers identify humidity deviations, equipment deterioration and maintenance requirements before they cause significant production interruptions. Intelligent controls can also adjust system operation according to actual process loads, outdoor conditions and production schedules.
Greater use of heat recovery, improved regeneration strategies and process-specific environmental controls will also shape future manufacturing facilities. Environmental data will become increasingly valuable for quality investigations, trend analysis and demonstrating that manufacturing conditions remain under control. Environmental-control engineering should therefore be incorporated into facility planning from the outset rather than addressed only after commissioning.
What is your message to pharmaceutical manufacturers who still view humidity control primarily as an HVAC issue?
Humidity control should be considered an investment in product quality and process efficiency, not merely an HVAC expense. Environmental conditions can influence raw materials, production consistency and the stability of finished medicines. Poor humidity control may result in powder-handling difficulties, production delays, inconsistent tablets, coating defects and avoidable quality investigations.
Manufacturers should involve their production, quality assurance, engineering and facility management teams in establishing critical process parameters and verifying that systems maintain the required conditions under actual production loads.
At Bry-Air, our approach is to understand each customer’s application before recommending an appropriate environmental-control technology. Ultimately, better humidity control means better control of the manufacturing process. It should therefore be regarded as both a business and quality priority in an industry where product quality and patient safety are paramount.